Prototype Molds
Prototype Injection Molds | Fast T0/T1 Sampling for NPI | Jeancen Mold
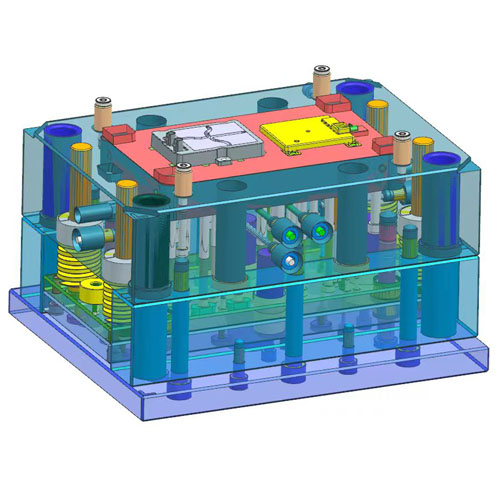
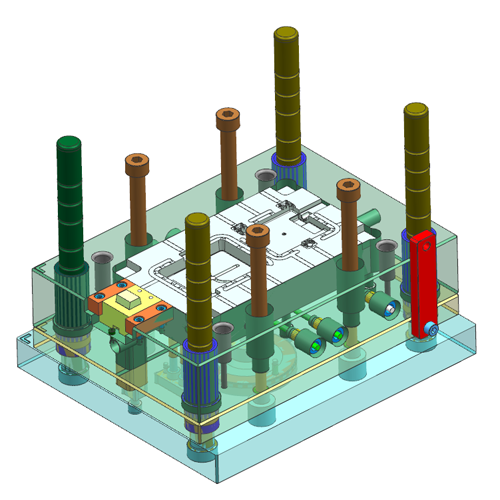
Rapid prototype injection molds engineered for reliable T0/T1 sampling and controlled iteration. Engineering review considers filling, venting, cooling, and ejection so you can validate fit, function, and assembly before production tooling.
Fast T0/T1 tooling for validation, pilot runs, and bridge production.
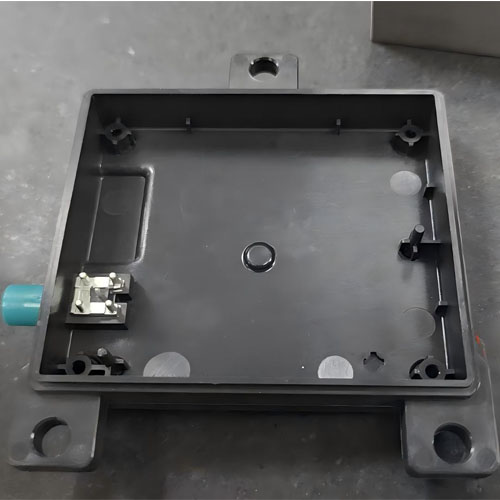
Prototype molds are built for speed without sacrificing the engineering fundamentals (filling, venting, cooling, ejection, and serviceability). Use this option when you need real injection-molded samples to validate fit, function, and assembly—before committing to long-life production tooling.
- Typical use cases: T0/T1 sampling, design validation, assembly fit checks, pilot runs, bridge tooling
- Initial review: feasibility notes and DFM risk flags based on the project information provided
What Is a Prototype Mold (Engineering Definition)
A prototype mold is optimized for speed-to-sample and controlled iteration:
- Fast build + fast iteration (modular inserts on risk areas)
- Predictable sampling results (stable gating/venting/ejection)
- Clear learning outcomes (what to change on the part or the tool, and why)
The goal is not “the cheapest mold.” The goal is a reliable learning cycle that reduces risk before production tooling.
What You Need to Send for an Initial Quote
- 3D CAD (STEP/IGES) + 2D drawing if available
- Material/resin + additives (GF, FR, UV, etc.)
- Appearance requirement (gloss/matte/texture, cosmetic side)
- CTQ dimensions & tolerance targets
- Expected volume (prototype qty, pilot run, annual projection)
- Target timeline (T0/T1 timing)
- Special requirements (insert molding, 2K, sealing, marking limits)
Key Cost Drivers
- Geometry risk (thin wall, shutoffs, undercuts, cosmetic faces)
- Cavity count & layout (single/multi/family)
- Runner & gating constraints (weld-line control, gate type)
- CTQ/tolerance intensity
- Surface finish requirement
- Iteration plan (need modular inserts or not)
Typical Lead Time & Process
- DFM timing: based on project scope and available data
- Tooling concept and quotation timing are confirmed once the project data and review scope are clear.
- Tool build timing is confirmed after DFM, tooling complexity, materials, and validation scope are reviewed.
- T0/T1 sampling is scheduled after mold assembly and readiness checks are completed.
Common Prototype Failure Modes & Fix Strategy
1) Short Shot / Burn Marks (Gas Traps)
Cause: insufficient venting, trapped air pockets
Fix: proactive venting layout, gate direction optimization, localized vent features
2) Flash at Shutoffs / Inserts
Cause: weak shutoff design, fit drift
Fix: tighten critical insert fit, strengthen shutoff design, define wear areas early
3) Ejection Marks / Part Damage
Cause: insufficient draft, poor ejection layout
Fix: ejection concept review, part-protection logic, draft recommendations
4) Warpage / Dimensional Drift
Cause: unbalanced cooling, residual stress
Fix: cooling balance improvements, DFM geometry notes, controlled process window
Parameters (Typical Tool Material Options)
Tool Material / Steel | Typical Use | Notes |
|---|---|---|
Aluminum tooling | Ultra-fast prototypes | Best when geometry is stable and the cosmetic target is moderate |
P20 | General prototype molds | Cost-effective for conventional materials and short runs |
718H | Demanding prototypes/bridge tooling | Better stability for longer pilot runs |
NAK80 | Cosmetic-focused prototypes | Good surface potential and consistency |
S136 / S136H | High polish/corrosion resistance | Ideal for PC/PMMA or high-gloss requirements |
Request an Engineering Review
Send your 2D/3D files (STEP) or product photos with key dimensions. We’ll review the information and confirm the appropriate next step.
- Contact / RFQ → Contact Us
- Email → info@jeancen.com
Not sure which one is right for you?
- Expect multiple revisions on clips/shutoffs/seal areas, and want faster changes? → Modular Prototype Molds
- Need stable low-volume production before final tooling is completed? → Bridge Tooling
- Appearance matters (cosmetic faces, gloss/texture boundaries, ejector witness control)? → Cosmetic Prototype Molds